
High-Precision Mold Components & Industrial Pneumatic Boosters
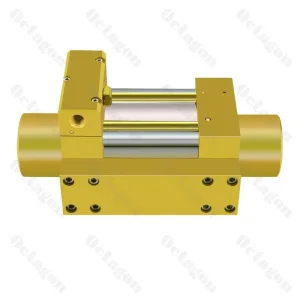
Explore initial core assemblies certified to CE safety thresholds, micro-machined to tolerances within ±0.002 mm with mirror finishes.







Macro Commercial Dynamics & EU Regulatory Landscape for Injection Tooling
Strategic insights into the shifts dominating multi-cavity injection molds, hot runner thermal efficiency, and European market CE conformity.
In modern polymeric manufacturing, the global injection molding market—surpassing an estimated valuation of USD 300 billion—is experiencing a profound technological pivot. Production cycles once measured in weeks are now constrained to microsecond tolerances, multi-material co-injections, and fully automated robotic demolding. The structural heart of this ecosystem is the precision-machined mold core, cavity, hot-runner nozzle, ejector mechanism, and synchronized pneumatic/hydraulic actuation hardware. Procurement managers across Europe, North America, and Southeast Asia face compounding operational challenges: minimizing cycle time, mitigating shear stresses, ensuring non-stop structural integrity, and strict adherence to mandatory European Union CE directives.
Securing a true CE Certification for Injection Molding Mold Parts is not merely an administrative exercise. For precision parts, in-mold automation units, and pneumatic-hydraulic intensifiers, conformity entails rigorous design verification against the EU Machinery Directive 2006/42/EC, the Pressure Equipment Directive (PED) 2014/68/EU, and harmonized safety benchmarks including EN ISO 12100:2010 and EN ISO 4414:2010. When custom tooling subsystems feature integrated electronic sensors, in-mold degaters, or pneumatic boost units, they must also satisfy the Electromagnetic Compatibility (EMC) Directive 2014/30/EU and the Low Voltage Directive (LVD) 2014/35/EU.
The global trade architecture has similarly evolved. Modern tier-1 automotive suppliers, medical device conglomerates, and renewable energy innovators no longer procure mold components as disjointed commodities. Instead, they demand integrated micro-mechanical systems backed by complete material traceability (EN 10204 Type 3.1 certification), zero-failure fatigue thresholds, and documented Environmental Product Declarations (EPD). Suppliers must demonstrate true Experience, Expertise, Authoritativeness, and Trustworthiness (E-E-A-T) by integrating advanced metallurgical engineering, optical multi-axis metrology, and in-depth risk assessments directly into standard operating procedures.
Advanced Material Science, Micro-Tolerancing & Surface Tribology
Engineering breakdown of alloy matrices, chemical surface treatments, and high-cycle mechanical resilience.
Alloy Selection & Heat Treatment
We machine tool cores and sliding components from certified Premium AISI H13, Stavax ESR (AISI 420 modified), and 1.2343 ESR steels. Through triple vacuum tempering and sub-zero cryogenic stabilization (-196°C), internal stresses are eliminated, achieving unified hardness between 52 to 58 HRC.
- Zero grain coarsening under thermal shock
- Traceable melt logs via EN 10204 3.1
PVD, CVD & Tribological Coatings
To withstand abrasive high-glass-fill resins (PA66-GF50, PEEK), core pins and ejector sleeves undergo multi-layer Diamond-Like Carbon (DLC), TiAlN, or CrN vapor deposition. This lowers coefficient of friction to μ < 0.1, preventing micro-galling and permitting dry (lube-free) cleanroom operation.
- Surface hardness exceeding 3000 HV
- Medical Class 10,000 cleanroom compliance
Sub-Micron Machining & Metrology
Components undergo finish grinding on Swiss Studer cylindrical grinders, Yasda 5-axis CNC jigs, and Makino high-speed oil-bath wire-cut EDM. Dimensional verification is guaranteed through Zeiss CMM optical-touch probes operating in ISO Class 7 temperature-controlled metrology suites.
- True circularity error < 0.001 mm
- Ra 0.05 μm optical mirror cavity finish
| Part Classification | Material Substrate | Hardness Profile | Dimensional Tolerance | Surface Roughness | CE & ISO Certification Compliance |
|---|---|---|---|---|---|
| Micro Core Pins & Punches | SKD11 / SKH51 / Vanadis 4 | 60 - 64 HRC Cryo | ±0.002 mm | Ra 0.05 μm | CE / EN ISO 12100 |
| In-Mold Cutting Cylinders | 42CrMo4 Alloy Steel / Al6061 Hard Coat | 48 - 52 HRC | ±0.005 mm | Ra 0.2 μm | PED 2014/68/EU |
| Die Casting Slide Blocks | AISI H13 / 1.2344 ESR | 48 - 50 HRC Nitrided | ±0.004 mm | Ra 0.2 μm | Machinery Directive |
| Gas-Liquid Booster Systems | 316L Stainless Steel & Aircraft Alloy | Pressure Tested to 800 bar | Standard NPT/G Porting | Ra 0.1 μm Piston Borings | CE / RoHS / EMC |
Mission-Critical Application Scenarios in High-Velocity Industries
Field deployment of precision tooling components across specialized sectors requiring zero operational tolerance for part flash, sink marks, or dimensional creep.
Automotive E-Mobility & ADAS
In-mold degating systems and optical mold inserts tailored for radar sensor radomes, high-voltage battery module connectors, and lightweight structural PA-GF housings requiring strict sealing integrity.
Medical Diagnostics & Microfluidics
Cleanroom compliant, DLC-coated micro core pins utilized to produce high-density pipette tips, IV connector assemblies, dialysis filtration casings, and surgical endoscope handles under ISO 13485 mandates.
Electronics & Smart Devices
Sub-micron mold cavities and ultra-compact ejector pin systems for wearable tech shells, high-definition display bezels, micro-pitch connectors, and optical waveguide arrays without parting-line flash.
Grid Energy Storage & Industrial Systems
High-voltage battery collection lines, heavy-duty industrial cabinet wire harnesses, and pneumatic air boosters installed on continuous-duty automated plastic stamping and molding production cells.
Overcoming Secondary Bottlenecks: Automated In-Mold Cutting Systems
A transformative macro solution eliminating manual sprue trimming, reducing cycle times by up to 25%, and standardizing gate finish quality.
In high-tonnage multi-cavity injection molding, secondary sprue removal represents one of the largest remaining drivers of operational waste, manual handling errors, and inconsistent cosmetic finishes. Traditional post-mold degating via manual snips, external automated laser stations, or downstream ultrasonic cutting induces micro-stresses, part contamination, and elevated labor overhead. Octagon's CE-certified In-Mold Cutting and Automation Solution resolves this fundamental structural limitation by executing sprue severance inside the closed tool during the cooling phase, before mold parting.
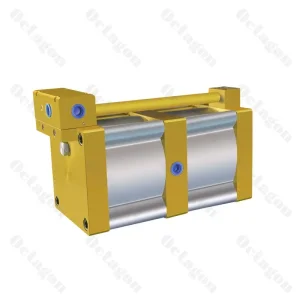
Powered by our synchronized High-Pressure Timing Control Cabinet and driven by pneumatic-hydraulic booster pumps (delivering 1,000 to 7,000 kgf of continuous linear shear force), the system actuates micro-shearing blades or valve-cutter pins at an exact millisecond timestamp within the mold cycle. The cut edge is pressed flush against the part profile while the polymer is still in a quasi-plastic thermal state, achieving a mirror-smooth gate scar with zero stress whitening, particulate generation, or micro-cracking.
15% – 25% Cycle Time Reduction
Trimming is performed concurrently within the mold cooling phase, removing post-processing cycle lags completely.
Zero Stress Whitening & Micro-Fissures
Shearing while the plastic remains warm prevents brittleness in polycarbonate (PC), PMMA, and filled polyamides.
100% Scrap Gate Separation
Finished parts and trimmed runners eject through separated automated channels directly into optical sorting bins.
Technology Roadmap & Future Outlook (2025 – 2035)
The progression of smart tooling: IoT sensor integration, conformal additive cooling, and closed-loop edge intelligence.
Phase 1 · Current Standard
Sub-Micron Subtractive Machining
Mainstreaming ±0.002 mm machining across standard tool steels; CE marked pneumatic booster stations; full EN 10204 3.1 material batch certification across all production lines.
Phase 2 · 2026-2028
Conformal Cooling DMLS Integration
Diffusion bonding and direct metal laser sintering (DMLS) of mold inserts with organic cooling channels, slashing cycle times by up to 35% on thick-wall structural moldings.
Phase 3 · 2028-2031
In-Cavity IoT Dynamic Sensors
Miniaturized piezo-electric pressure transducers and infrared melt front sensors embedded in core pins, broadcasting real-time viscosity and pressure gradients to MES systems.
Phase 4 · 2031-2035
Autonomous Edge-Adaptive Tooling
Closed-loop self-adjusting in-mold gate cutters that actively compensate for polymer batch viscosity deviations, preventing sink marks and flash autonomously via edge AI controllers.
Engineered Booster Units, Wire Harnesses & Tooling Accessories
Explore the remaining industrial configurations engineered for high reliability, automation, and CE-certified process compliance.





Frequently Asked Questions on CE Certified Mold Components
In-depth responses covering certification requirements, metallurgical tolerances, testing protocols, and custom OEM/ODM delivery.