
Featured Cabinet Harness & Pressure Systems
Discover our primary selection of pre-tested equipment cabinet wiring harnesses, air pressure booster pumps, and mold tooling components manufactured for industrial resilience.

High-Quality Equipment Cabinet Wiring Harness Manufacturers, Factory

ODM China Octagon SWP-7.5 Air Booster Pump Factory: Efficient Performance from Reliable Suppliers
CE Certification Octagon SWP-7.5 Air Booster Pump: High-Performance Solution from China Suppliers

High-Quality China Mold Inserts: Key Components from Reliable Suppliers and Factory for Precision Molding

High-Quality Automation Solution System Within The Mold Manufacturer, Product
OEM China Suppliers Octagon SWP-7.5 Air Booster Pump: High-Performance Factory Solution

Custom China Suppliers Factory Octagon SWP-02B-G Pneumatic Pump - Quality Design

CE Certification High-Precision Stamping Die Components from Top China Suppliers | Reliable Solutions
Engineering Equipment Cabinet Wiring Harness Architecture
Control cabinet environments demand uncompromising signal integrity, electromagnetic resilience, and dense cable routing. Here is how advanced harness manufacturing prevents operational downtime.
High-Density DIN Rail Topology
Modern electrical enclosures and PLC server cabinets face acute volumetric constraints. Our custom wire harness assemblies feature tailored breakout lengths, branch-specific heat shrink, and 3D CAD-routed trunks that directly align with standard 35mm DIN rails and industrial trunking channels, eliminating loose field loops and wire congestion.
Advanced EMI/RFI Shielding Integrity
Industrial cabinet switchgear produces significant inductive electromagnetic interference. We engineer harness solutions using tinned copper braided shielding (with up to 92% optical coverage), aluminum mylar wraps, and 360-degree connector backshell terminations to isolate sensitive RS-485, CANbus, Industrial Ethernet, and analog feedback signals from high-voltage motor drive cabling.
Thermal Dynamics & Flammability Safety
Enclosed equipment cabinets experience localized thermal hot-spots. Our cable harnesses incorporate specialized XLPE, PTFE, silicone, and Low Smoke Zero Halogen (LSZH) insulations rated from -40°C to +150°C. Complying with UL94 V-0 and VW-1 flammability classifications, every harness branch prevents smoke toxicity and flame propagation within enclosed server and automation racks.
Taiwan Engineering Rigor Coupled with China Production Scale
Since 2008, Octagon Precision Mold Co., Ltd. has bridged the gap between ultra-precision tooling engineering and scalable industrial manufacturing, serving global original equipment manufacturers across 60+ countries.
Sub-Micron Tooling Legacy
With an engineering heritage crafting mold parts to ±0.002 mm tolerances and Ra 0.05 mirror polishes, we apply identical mechanical tolerances to custom harness connectors, overmolds, terminal contact tooling, and high-pressure booster pump cabinets.
Integrated Component Sourcing
Our mainland China manufacturing facilities provide immediate access to the world's most concentrated ecosystem for copper drawing, specialized insulation polymer compounding, and authorized franchised connector distributors (TE, Molex, JST, Harting, Amphenol).
Automated Crimping & Stripping
Human assembly errors are eliminated through high-speed Komax automated wire cutting, stripping, and terminal crimping stations featuring micro-force crimp height measurement and digital cross-section analysis to guarantee joint conductivity.
Export-Grade Packing & DFM
Our 190+ personnel include senior R&D engineers offering comprehensive Design-for-Manufacturability (DFM) reviews, moisture-barrier vacuum packaging, modular loom labeling, and complete customs documentation for tariff-compliant global transit.
Engineering Parameters & Compliance Standards
Cabinet wiring harnesses produced by Octagon strictly adhere to international electromechanical standards, guaranteeing field safety, fire suppression, and long operational life cycles.
| Technical Parameter | Engineering Specification | Applicable Standards | Compliance Verification |
|---|---|---|---|
| Conductor Range | AWG 4/0 down to AWG 32 (Oxygen-Free High-Conductivity Copper / Tinned Copper) | ASTM B3, UL 758, IEC 60228 | 100% Spark Tested |
| Insulation & Jacketing | PVC, XLPE, Silicone Rubber, PTFE (Teflon), Polyurethane (PUR), LSZH | UL94 V-0, VW-1, CSA FT-1, RoHS 3 | Halogen-Free Certified |
| Dielectric Withstand Voltage | 300V to 3000V AC / DC dependent upon branch isolation requirements | IPC/WHMA-A-620 Class 3, IEC 60664 | Hi-Pot Continuity Verified |
| Operating Temperature | Continuous rating from -50°C to +150°C (-58°F to 302°F) | MIL-STD-202G, DIN EN 60068 | Thermal Cycling Tested |
| Shielding Effectiveness | >85% Tinned Copper Braid + Double-Sided Mylar Aluminum Foil Foil Shielding | EN 55032 / EN 55035 Class B EMC | EMC / EMI Compliant |
| Connector Termination | Crimp, Solder, Screw Terminal, IDC, Heavy-Duty Modular Industrial Inserts | DIN 41612, IEC 60352-2 | Tensile Pull-Force Certified |
Resolving Global Enterprise Procurement Bottlenecks
Tier-1 panel builders, machinery builders, and telecom integrators face mounting pressures from labor shortages and component lead times. Sourcing pre-tested wiring assemblies dramatically shortens the build cycle.
Reducing On-Site Cabinet Assembly by 60%
Manual point-to-point panel wiring on factory floors is notoriously labor-intensive, error-prone, and expensive. Transitioning to pre-fabricated, point-to-point tested equipment cabinet wiring harnesses converts days of manual wire cutting, labeling, and crimping into a quick plug-and-play assembly process.
Mitigating Supply Chain Disruptions
Global supply chain volatility can hold up an entire multimillion-dollar automation shipment due to a single delayed connector. Octagon’s dual engineering footprint (Taiwan & Mainland China) maintains verified second-source component equivalency lists for terminals, wire, and conduits without compromising functional specs.
Lowering Total Cost of Ownership (TCO)
The total cost of a harness is not simply the unit price. It includes field failure warranties, rework labor, and commissioning downtime. By subjecting 100% of our harnesses to automated Cirris electrical continuity and high-voltage breakdown checks before crating, we drive initial customer acceptance rates to 99.8%.
Industrial Application Scenarios for Cabinet Wiring Harnesses
From extreme outdoor climate energy cabinets to cleanroom semiconductor tool control racks, our harnesses operate seamlessly across diverse operating environments.
Industrial Automation & PLC Consoles
Main control cabinets for CNC mills, automated packaging lines, and robotics cells. Carries multi-conductor digital 24V I/O, safety interlocks, and servo feedback lines with high-flexibility grouping.
BESS Energy Storage Power Cabinets
Grid-scale Battery Energy Storage System (BESS) high-voltage distribution racks. Engineered to handle large ampacities, temperature sensor loops, and isolated communication bus backbones under cyclic thermal stress.
Edge Data Centers & Telecom Racks
High-density 19-inch server rack enclosures. Features color-coded power distribution harnesses, fan tray power assemblies, and optical fiber-protective conduits optimized for unimpeded cabinet airflow.
Semiconductor & Medical Enclosures
Vacuum chamber controllers and diagnostic equipment cabinets. Assembled in cleanroom settings with ultra-low outgassing fluoropolymer cables, gold-plated contacts, and anti-static outer wraps.
Technological Horizons & Next-Gen Cabinet Trends
The wiring harness manufacturing sector is transitioning from traditional handcrafted wiring to AI-assisted digital twins, robotic harnessing, and intelligent embedded diagnostics.
Smart Harnesses with Embedded RFID
Future control cabinets increasingly employ smart harnesses fitted with near-field RFID micro-chips and 2D matrix data labels. Technicians scanning a connector branch instantly pull up complete schematics, terminal pinout configurations, manufacturing test logs, and revision histories on augmented-reality maintenance glasses.
Modular Quick-Disconnect Architectures
Traditional terminal blocks are rapidly yielding to standardized push-in, heavy-duty modular rectangular connectors (e.g., Harting Han-Modular, Phoenix Contact). Our harnesses utilize modular blind-mating frames that allow field maintenance engineers to swap sub-cabinet electronics modules within seconds without handling individual conductors.
Automated Optical Inspection (AOI)
Using advanced AI-powered computer vision and multi-axis camera rigs, harness layout stations verify wire strip lengths, terminal crimp geometry, heat shrink positioning, and pin assignment accuracy down to 0.05 mm, surpassing manual visual inspection limits.
Questions Global Procurement & Engineers Ask
Detailed answers regarding manufacturing tolerances, quality assurance procedures, material compliance, and minimum order requirements.
What quality standards govern your cabinet harness manufacturing?
We manufacture strictly in compliance with IPC/WHMA-A-620 Class 2 and Class 3 (commercial, industrial, and high-reliability critical service). Our production facilities operate under ISO 9001:2015 quality management procedures, and harness designs are built to achieve UL, CE, RoHS, and REACH international approvals.
Can you cross-reference hard-to-source connector brands?
Yes. While we regularly build using authentic original components from TE Connectivity, Molex, JST, Harting, Amphenol, and Hirose, our senior engineering team can provide drop-in form-fit-function equivalents from verified domestic manufacturers to reduce costs by 25-40% and cut lead times significantly.
How do you test and validate completed cabinet harness assemblies?
Every harness assembly undergoes 100% computerized electrical testing using Cirris test analyzers. We test for pinout continuity, branch miswires, short circuits, high-voltage breakdown (Hi-Pot up to 3000V AC), and insulation resistance (>100MΩ). Mechanical crimp pull-force tests are recorded every production shift.
What file formats are required for an OEM/ODM quote?
We accept complete wiring schematics, pinout charts, and dimensional drawings in PDF, DWG, and DXF formats. For complex 3D cabinet routing, we encourage 3D CAD files (STEP, IGES, SolidWorks) along with your preferred Bill of Materials (BOM) specifying wire gauges, connector part numbers, and labeling protocols.
What are your typical production lead times and Minimum Order Quantities (MOQs)?
We support high-mix, low-volume (HMLV) industrial orders as well as large-scale production runs. Prototyping and first-article samples typically ship in 1 to 2 weeks following drawing sign-off. Volume production runs take 3 to 4 weeks depending on specific connector availability.
How do you resolve EMI interference between power and signal lines?
We employ internal geometric segregation, twisted pair configurations for differential signals, dual-layer foil-plus-braid shields, and grounded internal metallic divider shields within the main harness trunk. Grounding wires and drain wires are terminated directly to chassis studs or connector shielding backshells.
Industrial Pneumatic & Cabling Systems Portfolio
Explore our secondary line of industrial cable harnesses, high-efficiency gas-liquid boost pumps, and precision tooling components backed by 45+ international patents.

OEM SWB-100S Series Pump - High-Efficiency Gas-Liquid Booster from China Suppliers

OEM Cooling Fan Cable Harness - China Factory Suppliers for Computers, Automotive & Equipment

ODM SWP-05-G Air Booster Pump from China Suppliers - High Efficiency Factory Solution

ODM Octagon SWP-02A-G Air Booster System - Advanced Pneumatic Technology from China
ODM Mold Inserts from China: Top Suppliers & Factory for Precision Components
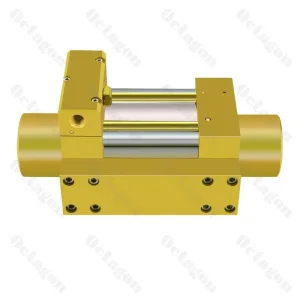
ODM Octagon SWB-80D Booster Pump Factories, Exporters Industrial Boosting Solution

High-Quality China SWP-05 Air Booster Pump: User-Friendly Efficiency from Suppliers