

Pressure Boost
Strategic precision mold components, non-standard processing, and in-mold automation supporting Vietnam's premier economic cluster.
Ho Chi Minh City (HCMC) and its adjacent industrial corridors—Dong Nai, Binh Duong, and Long An—represent the epicenter of Vietnam's rapid industrialization. Over the past decade, global electronics giants, automotive tier-1 suppliers, and precision medical device manufacturers have transformed the Southern Key Economic Zone (SKEZ) into a high-throughput production base. However, the rapid expansion of plastic injection molding, high-pressure die casting (HPDC), and progressive metal stamping lines has exposed a critical gap: the availability of localized, ultra-precision mold parts that can withstand demanding 24/7 duty cycles.
Local tooling infrastructure in HCMC is developing fast, yet high-wear non-standard components—such as micro-ejector pins, precision slide retainers, beryllium copper inserts, and high-frequency in-mold cutting units—often face lead-time and tolerance bottlenecks. To maintain rapid cycle times and eliminate micro-burrs, modern factories across Saigon Hi-Tech Park (SHTP) and VSIP (Vietnam-Singapore Industrial Park) require tier-1 mold suppliers capable of consistent sub-micron machining accuracy (±0.002 mm), specialized vacuum heat treatments, and integrated fluid-power pneumatic booster systems.
Direct logistical air and ocean lanes connecting our advanced manufacturing hubs in southern China with Cat Lai Port and Tan Son Nhat Airport deliver production-critical components in as little as 3 to 5 business days, safeguarding against line stoppages.
Every core insert, punch pin, and hydraulic cylinder utilizes certified tool steels—including SKD11, SKD61, DC53, and HAP40 powdered metallurgy—with full spectral inspection reports to ensure exceptional fatigue resistance.
Engineered to elevate injection molding press performance and pneumatic stability for Ho Chi Minh City manufacturing plants.



How combining advanced Taiwanese engineering principles with scalable Chinese industrial infrastructure creates unprecedented procurement value.
Our manufacturing facilities operate in the world's most integrated precision engineering corridors. Raw material sourcing, ultra-deep cryogenic treatment, titanium carbo-nitride (TiCN) PVD coating, and mirror wire EDM are co-located within a 20-kilometer radius, slashing cycle times by up to 60% compared to Western and domestic tooling shops.
By utilizing continuous five-axis machining centers (Makino, Sodick, GF Machining Solutions), our shops deliver mold bases, slide cores, and non-standard punch inserts at tolerances of ±0.002 mm without charging the exorbitant premiums common to European or Japanese niche fabricators.
Enterprises running production in Ho Chi Minh City leverage our direct supply to bypass multi-layer distributor markups. High-longevity mold components reduce scheduled downtime, minimize gate vestige defects, and prolong the life of expensive injection molds from 500,000 to over 2,000,000 cycles.
| Performance Metric | Standard Market Parts (HCMC Domestic) | Octagon Precision Engineering Spec | Operational Impact for Toolmakers |
|---|---|---|---|
| Dimensional Tolerance | ±0.010 mm ~ ±0.020 mm | ±0.002 mm (Micro-ground) | Zero flash, airtight cavity seals, interchangeable inserts |
| Surface Roughness (Ra) | Ra 0.4 ~ 0.8 μm | Ra 0.05 ~ 0.2 μm (Mirror finish) | Reduces friction, enables smooth part ejection without release agents |
| Steel Hardness & Purity | HRC 48-52 (Generic D2/SKD) | HRC 58-64 (Vacuum Quenched DC53/ASP23) | Triple wear life against abrasive glass-filled resins (PA66-GF30) |
| In-Mold Cutting Integration | External manual degating | Synchronized Booster Pneumatic Units | Saves 3-8 seconds per shot; eliminates secondary labor |
Custom-engineered mold components and pneumatic boost systems deployed in leading manufacturing facilities throughout southern Vietnam.
Supplying high-density multi-cavity connector mold inserts, guide pins, and high-definition connection harnesses for micro-electronic enclosures, optic sensors, and smart device packaging manufactured by global tech leaders in District 9.
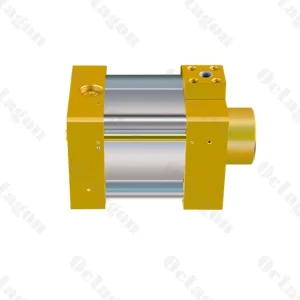
Delivering high-force gas-liquid booster pumps (SWB/SWP series) for in-mold gate shearing of automotive interior trims, bumper brackets, and HVAC vents in VSIP I/II and Bien Hoa Industrial Zones, eliminating cosmetic post-trim blemishes.
Precision stainless steel (SUS420/S136 ESR) core pins and medical wiring harnesses fabricated for cleanroom-grade diagnostic housings, syringe molds, and EV battery energy storage collection assemblies under stringent ISO 13485 quality protocols.
The precision injection and die-casting mold sector is moving rapidly away from manual, labor-heavy post-processing. Modern manufacturers in Ho Chi Minh City are prioritizing three fundamental technological shifts:
Traditional gate clipping incurs significant manual labor and uneven part edges. Our pneumatic-hydraulic booster cylinders and timing control cabinets deliver 1,000 to 7,000 kgf of shearing force within the mold while the tool remains locked under clamp tonnage, cleanly severing pinpoint, submarine, or tunnel gates before mold opening.
Incorporating Ampcoloy or beryllium-copper inserts inside deep-rib cavities accelerates cooling times by up to 35%. When machined to ±0.002 mm and coupled with conformal cooling channels, cycle times in HCMC factories drop dramatically.
Adopting global DIN/ISO/MISUMI/HASCO interchangeability allows multi-plant manufacturers across Southeast Asia and China to share spare tooling inserts seamlessly without custom fitting or manual stone lapping.
When vetting an overseas precision mold parts supplier for Vietnamese production lines, international procurement teams evaluate four core criteria:
Technical answers regarding tolerances, metallurgy, air booster pumps, logistics, and non-standard mold machining.
For standard mold base components, ejector sleeves, and non-standard machined core inserts, standard manufacturing lead time ranges from 5 to 10 working days. Air express shipments (via DHL/FedEx/SF Express) to Ho Chi Minh City, Binh Duong, and Dong Nai typically take 2 to 4 days, while consolidated sea freight via Cat Lai Port takes 7 to 10 days.
We maintain constant-temperature machining facilities equipped with Sodick oil-dielectric wire EDM, Makino graphite electrode milling, and Okamoto precision surface grinders. In-process inspection is performed using non-contact optical projectors, Mitutoyo linear height gages, and Zeiss CMMs calibrated to international traceability standards.
Yes. While we supply standard mold components compliant with MISUMI, DME, and HASCO specifications, over 65% of our production consists of custom non-standard mold parts engineered strictly to customer CAD models (STEP/DWG), including complex slides, angled lifters, custom sprue bushings, and high-pressure die casting shot sleeves.
Standard shop pneumatic lines operate at 5 to 7 bar, which is often insufficient to trigger heavy mechanical locks, core-pulling cylinders, or in-mold cutting blades. Octagon SWP and SWB booster pumps multiply input compressed air into stable hydraulic pressures reaching several hundred bar without requiring an expensive external hydraulic power unit.
Every shipment includes a full certificate of analysis (COA), raw material spectral heat-treatment certificates, dimensional CMM inspection reports, and Certificate of Origin (Form E or standard CO) to support smooth Vietnamese customs clearance under applicable free-trade agreements.
Explore our full range of wire harnesses, precision die-cast mold components, and pneumatic booster systems.





Accelerate your injection molding, die casting, and wire harness production in Ho Chi Minh City. Connect directly with our senior tooling engineers to review tolerances, materials, and CAD drawings.