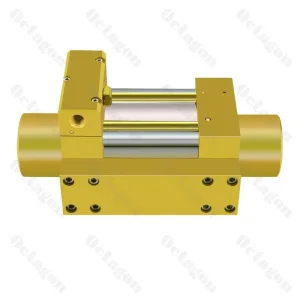
Industrial Systems for Optimized Pressure Amplification
Engineered for clean operating pressure transfer, continuous duty cycles, and integration into automated mold tooling, machine fixturing, and high-force pneumatic presses.


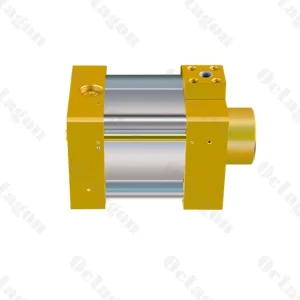




Pneumatic Cylinder Operating Pressure Dynamics & CE Compliance
In modern automated tooling, pneumatic actuators and boost cylinders are subjected to rigorous cyclical mechanical stress. Achieving true compliance with European directives requires an in-depth understanding of operating pressure tolerances, proof pressure calculations, and fluid power safety standards.
Operating vs. Proof Pressure
Standard industrial air cylinders operate within 0.4 to 0.8 MPa (4 to 8 bar), while high-force boost assemblies achieve working pressures of 1.5 to 7.0 MPa. In compliance with EN ISO 4414, our manufacturing establishes proof pressure at a minimum of 1.5× nominal pressure and burst pressure at 4.0× design thresholds to guarantee physical enclosure integrity.
- Hydrostatic burst safety factor ≥ 4:1
- Cyclic fatigue qualification > 5M strokes
- Zero slip-stick dynamic seal friction
PED 2014/68/EU & Machinery Directive
Cylinders and air booster tanks whose pressure-volume product (P·V) exceeds statutory European thresholds fall under the Pressure Equipment Directive (PED 2014/68/EU). We implement Harmonized Standard assessments under Module B+D, ensuring compliance with Machinery Directive 2006/42/EC for automated mold integration.
- EN ISO 4414 Pneumatics Safety Verification
- EN ISO 13849-1 PL-d / PL-e Ready Components
- Traceable 3.1 Material Test Reports
Sealing Science & Tribology
High operating pressures accelerate micro-extrusion of elastomeric seals. Octagon employs custom Parker/NOK polyurethane (PU) and fluorocarbon (FKM) piston rings engineered for low break-away friction, combined with hard-anodized 6061-T6 aluminum barrels honed to an internal surface roughness of Ra 0.05 to 0.2 μm.
- Mirror internal bore finish: Ra 0.05–0.2 μm
- Machining concentricity tolerance ±0.002 mm
- Self-lubricating PTFE/bronze guide bushings
| Cylinder Series / Class | Bore Range (mm) | Rated Operating Pressure | Peak Proof Pressure | Output Force Range (kgf) | CE Regulatory Standard |
|---|---|---|---|---|---|
| SWP High-Ratio Air Booster | Ø40 – Ø160 | 0.2 – 1.0 MPa (Air Input) | 1.6 MPa | Up to 3,500 kgf | 2006/42/EC, EN ISO 4414 |
| SWB Gas-Liquid Booster Pump | Ø80 – Ø200 | 0.3 – 0.8 MPa to 70 MPa (Hyd.) | 105 MPa (Liquid Side) | 1,000 – 7,000 kgf | PED 2014/68/EU, ISO 19879 |
| In-Mold Cutting Actuator | Ø25 – Ø100 | 0.6 – 3.5 MPa (Intensified) | 5.5 MPa | 800 – 5,200 kgf | EN ISO 13849-1 Cat 3 |
| Precision Micro-Tie Rod Cylinder | Ø16 – Ø63 | 0.15 – 1.2 MPa | 1.8 MPa | 120 – 1,800 kgf | EN 60204-1, RoHS 2011/65/EU |
Why Global Tier-1 Buyers Choose Our China Factory
Established in 2008 with headquarters in Taoyuan City, Taiwan, Octagon Precision Mold Co., Ltd. operates state-of-the-art production facilities in mainland China. We unite Taiwan's precision tooling methodologies with mainland China's robust industrial supply chain and rapid turnaround capabilities.
Cost-to-Precision Ratio
Through domestic metal raw material sourcing, automated 5-axis CNC cell machining, and integrated mold-base tooling, our mainland plant slashes capital expenditure for European and North American buyers by 35% to 50% without compromising micron tolerances.
190 Specialists & R&D
Our engineering workforce comprises 190 dedicated specialists, including senior fluid mechanics and tooling engineers with over a decade of hands-on R&D tenure. Drawing reviews and 3D flow simulations occur within 24 hours of technical RFQ submission.
Comprehensive Quality Gates
From optical coordinate measuring machines (CMM) to pneumatic burst decay test stands and helium leak spectrometry, 100% of cylinder housings and booster circuits undergo individual serial-numbered pressure testing prior to export dispatch.
Scalable Customization
Whether your enterprise requires specialized non-rotating piston rods, extreme chemical environment Viton sealing, or custom pressure ratio ratios (such as 2.5:1, 4:1, or 80:1), we support agile OEM/ODM low-volume pilots to massive production runs.
Emerging Trends in High-Pressure Fluid Power
Global decarbonization targets and smart automation demand cylinders that deliver higher force density with lower baseline air consumption. Discover the macro solutions driving modern equipment builders.
Decentralized Point-of-Use Boosting
Rather than operating entire plant air compressor networks at energy-wasting 10–12 bar, world-class automotive and stamping facilities run central loops at 5–6 bar. They install Octagon SWP air booster pumps directly at individual workstations, dramatically slashing energy overhead by up to 28%.
IO-Link & Digital Pressure Feedback
Smart factories integrate cylinders with micro-piezoelectric sensors and IO-Link interfaces. Real-time chamber pressure tracking detects seal degradation, internal bypass leakage, and pneumatic drop spikes before catastrophic machine stoppages can occur.
Cleanroom & Zero-Oil Hydraulics
Medical molders and cleanroom electronics manufacturers are actively replacing conventional hydraulic power units with gas-liquid booster cylinders and air amplifiers, eliminating toxic oil mist, pipe leakage, and environmental cleanroom cross-contamination.
Engineered for Demanding Industrial Environments
Across thousands of plant floors worldwide, Octagon pneumatic operating pressure systems deliver uncompromising precision where downtime is unacceptable.
In-Mold Degating & Trimming
Operating at boosted hydraulic forces of 1,000 to 7,000 kgf within compact injection molds. Actuates cutting blades while the mold remains clamped under temperature, eliminating manual secondary gate trimming and producing flawless automotive optical parts.
Automotive Stamping Clamping
Providing sustained, vibration-resistant clamping pressure across automated transfer press lines. Ensures sheet metal stamping dies remain absolutely stationary during high-frequency impact cycles with zero pressure creep.
Medical Device Cleanrooms
Powering ultrasonic welding and micro-assembly of dialyzers and syringe components. Uses dry, unlubricated filtered air cylinders certified to cleanroom standards without particle shedding or lubricant blow-by.
Battery Pack & ESS Assembly
Executing continuous pressure-controlled swaging and wiring harness terminal crimping in battery energy storage systems (BESS). Delivers micron-repeatable stroke depth regardless of pneumatic supply fluctuations.
Strategic Procurement Guide for Global Enterprise Buyers
When selecting an OEM/ODM supplier for pressure-critical pneumatic cylinders and boosters, multinational purchasing directors evaluate far more than unit purchase price.
Total Cost of Ownership (TCO)
Premature seal failure costs thousands of dollars in unplanned downtime. Octagon cylinders use proprietary micro-honed surfaces and self-compensating rod wipers that multiply maintenance intervals by 3.5× compared to standard catalogue components.
Traceability & CE Dossiers
Every shipment to the EU includes full technical compliance files: Declarations of Conformity, PED material certs (EN 10204 3.1), burst calculations, and risk mitigation protocols conforming to the strict mandates of the EU Machinery Regulation.
Export Packing & Supply Stability
Machined cylinders and electronic harness connectors are shipped in moisture-barrier anti-static packaging with internal nitrogen purging for overseas sea freight, guaranteeing zero corrosion on critical mirror-bore surfaces upon arrival.
Frequently Asked Questions on Operating Pressure & Compliance
Direct answers to core mechanical, compliance, and custom configuration questions raised by senior automation engineers and international sourcing specialists.
What is the maximum operating pressure for your air booster systems?
Our standard SWP air-driven booster series amplifies standard shop air (0.3 to 0.8 MPa) by factors of 2:1 up to 5:1, yielding air pressures up to 4.0 MPa. For extreme applications, our SWB gas-liquid booster pumps drive fluid output pressures up to 70 MPa (700 bar / 10,150 PSI) utilizing only compressed air drive.
How does Octagon ensure CE certification compliance on pressure equipment?
Every cylinder barrel, end cap, and booster pressure chamber undergoes finite element analysis (FEA) and hydrostatic burst pressure proof testing at 1.5× rated design limits. Pressure equipment adhering to Directive 2014/68/EU (PED) is inspected under notified body audits with complete EN 10204 3.1 material traceability.
Can you provide custom stroke lengths and mounting styles for tight tooling molds?
Yes. Because we engineer both precision mold parts and actuators in-house to ±0.002 mm tolerances, we customize stroke lengths from 5 mm to 2,000 mm, non-standard metric threads, compact manifold blocks, high-temperature FKM fluorocarbon seals, and specialized mounting flanges (ISO 15552, ISO 6432, and custom OEM prints).
What is the internal surface finish of Octagon pneumatic cylinder tubes?
Our cold-drawn seamless aluminum and stainless steel barrels undergo multi-step diamond burnishing and honing, achieving an internal mirror surface roughness of Ra 0.05 to 0.2 μm. This exceptionally low roughness prevents premature seal wear, cuts friction by 40%, and enables smooth actuation even at low speeds.
What documentation accompanies every international OEM batch shipment?
International shipments include a Certificate of Conformity (CE), dimensional inspection report measured by CMM, hydrostatic pressure proof test certificates, raw material chemical and mechanical test reports, and English maintenance manuals with full bill-of-materials and seal kit part numbers.
How do air-driven boosters compare with electric hydraulic power units (HPUs)?
Air-driven booster pumps stall automatically when the target high pressure is reached, holding dead-end pressure indefinitely without consuming electrical energy or generating heat. Unlike HPUs, they require no cooling water loops, produce zero electrical spark hazards, and eliminate dirty hydraulic oil leaks.
Specialized Booster Pumps, Harnesses & Mold Components
Explore our full OEM and ODM production capabilities across high-pressure fluid units, electronic equipment cabinet harnesses, and precision mold components.