
OEM Precision Injection Mold Supplier & Product Solutions
High-Precision Mold Tooling, Sub-Micron Core Inserts, In-Mold Cutting Automation, and Multi-Domain Wire Harness Integration for Mission-Critical Engineering.
Featured Industrial Equipment • Batch A
Standardized mold components, high-efficiency pneumatic/gas-liquid pressure boosters, and advanced harness nodes manufactured to micron-grade tolerances.







Global Landscape • OEM Precision Injection Tooling
Navigating the transition toward multi-cavity micromolding, conformal thermodynamic management, and closed-loop process automation across international supply chains.
The global precision injection molding sector has shifted from basic tooling assembly to a highly integrated engineering discipline. Modern tier-one programs within automotive electrification (EV), medical microfluidics, and consumer telecommunications demand dimensional repeatability down to sub-micron thresholds. The rapid miniaturization of multi-pin interconnects, smart sensors, and thin-wall electronic enclosures requires precision injection mold makers to synthesize extreme metallurgy, advanced thermal balancing, and ultra-high-speed pneumatic/gas-liquid pressure systems.
As an industry authority originating in Taoyuan, Taiwan with scalable manufacturing across mainland China, Octagon Precision Mold Co., Ltd. (founded in 2008) operates at the nexus of high-precision component fabrication and intelligent system integration. Employing over 190 senior specialists with an average engineering tenure exceeding 10 years, Octagon manages the complete production lifecycle: from raw substrate qualification (such as premium SKD11, SKD61, and high-purity tungsten carbide) to multi-axis CNC micro-milling, wire EDM, and synchronized in-mold degating automation.
Industrial Solutions • Integrated Ecosystem
Overcoming cycle bottlenecks, gate degradation, and thermal distortion through multi-disciplinary toolmaking and synchronized pneumatic boosters.
In-Mold Degating & Automation
Eliminate downstream secondary gate-trimming and manual post-processing. Our patented in-mold cutting automation systems leverage high-pressure timing cabinets (1,000 to 7,000 kgf dynamic output force) to execute micro-gate shear while the mold remains clamped, reducing overall cycle times by up to 28% and ensuring zero cosmetic burrs.
Sub-Micron Tooling & Mold Parts
Fabrication of critical mold cores, cavitation inserts, precision slider guides, and sprue bushings holding dimensional tolerances to ±0.002 mm. Enhanced with physical vapor deposition (PVD/DLC) surface coatings, our components achieve mirror surface finishes of Ra 0.05–0.2 μm, extending mold service life beyond one million cycles.
Fluid & Pneumatic Amplification
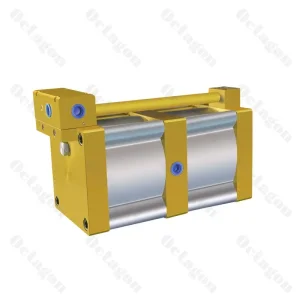
Engineered to overcome industrial facility pressure fluctuations. Octagon’s SWP and SWB series gas-liquid booster pumps amplify standard factory line air into continuous, ultra-high-pressure vectors. Essential for pneumatic ejector banks, core-pulling actuators, leak testing stations, and high-pressure gas-assisted injection molding.
Mission-Critical Applications • Cross-Sector Integration
Providing engineered synergy where mechanical mold precision converges with mission-critical wiring harness architecture.
Electric Mobility & Energy Storage (ESS)
Automated multi-cavity injection molds for battery module terminal frames, combined with custom heavy-gauge battery collection lines, signal sampling harnesses, and flame-retardant connectors tested under extreme thermal gradients.
Medical Diagnostics & Microfluidics
Cleanroom-certified plastic mold parts, sterile luer-lock connectors, and biocompatible medical wiring harnesses produced under strict ISO traceability standards, ensuring zero particulate contamination and zero signal jitter.
Display Tech & High-Speed Audio/Visual
High-definition screen connection cable harnesses, high-frequency low-loss transmission lines, and precision mold frames for ultra-thin consumer monitors, automotive HUDs, and acoustic component enclosures.
| Performance Parameter | Octagon Precision Tier | Conventional Industry Baseline | Engineering Benefit |
|---|---|---|---|
| Machining Tolerance | ±0.002 mm (±2 μm) | ±0.010 mm to ±0.020 mm | Eliminates parting line flash; enables complete interchangeable modularity. |
| Mold Cavity Surface Roughness | Ra 0.05 – 0.2 μm (Optical Mirror) | Ra 0.8 – 1.6 μm | Minimizes demolding shear stress; prevents cosmetic micro-scratches. |
| In-Mold Cutting Output Force | 1,000 – 7,000 kgf (Real-time HMI) | External manual shearing | Clean vestige cut; shortens overall cycle times by up to 28%. |
| Substrate Metallurgy | Certified Assab / Daido / Premium Tungsten | Generic tool steels | Extends tooling longevity past 1,000,000 continuous injection shots. |
Technology Roadmap • Next-Gen Mold Engineering
Anticipating the technological disruptions of Industry 4.0 through digital metallurgy, additive conformal cooling, and edge-computing sensors.
Additive Conformal Cooling
Transitioning from traditional straight-drilled cooling channels to DMLS (Direct Metal Laser Sintering) 3D-printed tool inserts. Conformal water lines follow complex cavity contours uniformly, eradicating localized hot spots and reducing thermal warpage in crystalline polymers by 45%.
IoT-Enabled Cavity Telemetry
Embedding micro piezoelectric pressure and infrared temperature transducers directly behind mold cavity inserts. Real-time feedback transmits thermodynamic telemetry to the molding press, dynamically balancing injection velocity to eradicate short shots or over-packing.
Sustainable Bio-Resin Processing
Engineering specialized mold gate geometries and wear-resistant coatings to accommodate abrasive bio-based and highly recycled post-consumer resins (PCR), ensuring that environmental compliance never compromises precision or dimensional stability.
Technical FAQ • Procurement & Engineering Insights
Direct technical answers addressing the critical parameters engineering directors, mold designers, and global procurement managers evaluate during vendor qualification.
What specific dimensional tolerances and surface finishes does Octagon guarantee on precision injection mold parts?
Octagon Precision Mold operates a climate-controlled CNC, EDM, and grinding facility that reliably achieves dimensional machining tolerances down to ±0.002 mm (±2 μm). For optical, medical, or high-aesthetic applications, we deliver mirror surface finishes ranging from Ra 0.05 to Ra 0.2 μm using diamond hand-lapping alongside high-speed fluid micro-finishing. Every shipment is accompanied by comprehensive CMM (Coordinate Measuring Machine) and optical measurement reports.
How does an in-mold cutting automation system function, and what cycle time reductions can be expected?
Our in-mold cutting automation system utilizes a dedicated high-pressure timing control cabinet connected to internal hydraulic/pneumatic micro-cylinders within the tool base. The system triggers precision cutter pins at a precise millisecond during the packing or cooling phase while the mold remains clamped under tonnage. This detaches the runner system instantly, resulting in cycle time reductions between 15% and 28%, eliminating secondary human labor, preventing mechanical stress damage, and yielding pristine gate vestiges.
How does Octagon coordinate manufacturing and quality assurance across its Taiwan and Mainland China facilities?
Octagon maintains its corporate headquarters, primary R&D engineering, and high-complexity prototype validation centers in Taoyuan, Taiwan, while operating scalable high-volume production facilities in mainland China. Both facilities follow identical ISO-certified operating procedures and ERP management. Our Taiwanese master toolmakers oversee drawing reviews, DFM (Design for Manufacturability) analyses, and final QA audits, ensuring clients receive European-tier precision combined with competitive volume scalability.
Can Octagon manufacture custom wire harnesses alongside precision mold components for integrated electro-mechanical assemblies?
Yes. Octagon is uniquely positioned as a multi-domain OEM/ODM manufacturer. In addition to high-precision injection tooling, stamping dies, and booster pumps, we engineer application-specific wire harnesses: including high-voltage energy storage (ESS) collection lines, IP68-rated waterproof harnesses, medical diagnostics cabling, and high-definition screen LVDS/eDP assemblies. This dual capability allows tier-one OEMs to source complete overmolded electronic sub-assemblies from a single accountable manufacturer.
What is the standard procedure and lead time for initiating an OEM/ODM precision injection mold project?
Projects initiate with an engineering review of customer 2D/3D CAD models (STEP, IGES, DWG) and mold flow analysis. Our engineering team returns a complete DFM proposal within 24 to 48 hours, highlighting parting lines, gate positioning, ejection mechanisms, and cooling channels. Standard prototype tooling lead times range from 15 to 25 business days, while multi-cavity production tooling typically takes 30 to 45 business days, concluding with full T1 sampling, dimensional inspection reports, and process parameter sheets.
Featured Industrial Equipment • Batch B
Specialized non-standard die-casting components, precision sprue bushings, in-mold automation controllers, and IP68 waterproof connection systems.




