
High-Efficiency Air Booster Stations for German Automation
Direct plug-and-play pneumatic pressure amplification systems engineered for continuous industrial duty, local line-pressure boosting, and energy-conscious factory layouts.

Octagon SWP-02A-G Air Booster System (Germany Standard)
Complete skid-mounted booster package with integrated air accumulator tank, regulator, and dual DIN-standard pressure monitoring for localized machinery lines.
Inquire Specs & RFQ
Custom SWP-7.5-G High-Ratio Air Booster Pump for Germany
Heavy-duty pneumatic amplifier designed for heavy mechanical presses, hydraulic valve pilot actuation, and high-tonnage sheet metal stamping fixtures.
Inquire Specs & RFQ
OEM SWP-02A-G-T Tandem Air Booster Pump (German Machining)
Dual-piston tandem architecture providing uninterrupted volumetric displacement, ideal for multi-axis CNC machine tool clamping and continuous leak test rigs.
Inquire Specs & RFQ
ODM Octagon SWP-02A Dynamic Air Booster (Industry 4.0 Ready)
Pure pneumatically operated intensifier requiring zero electrical connection, safe for ATEX zones and automated production lines across Bavaria and Baden-Württemberg.
Inquire Specs & RFQThe German Compressed Air Landscape: Energy Costs vs. Point-of-Use Pressure
An engineering assessment of how German industrial enterprises solve high industrial electricity tariffs and ISO 50001 compliance through localized pneumatic boosting.
1. The Energy Efficiency Dilemma in German Industrial Plants (EnMS ISO 50001)
In Germany's manufacturing corridors—spanning Stuttgart's automotive engineering, Munich's advanced mechatronics, and North Rhine-Westphalia's heavy industrial tooling—plant directors face some of the highest industrial energy tariffs in Europe. Compressed air is notoriously the most energy-intensive factory utility, often consuming 10% to 20% of an entire manufacturing facility's electrical draw. Historically, when a specific production process (such as a high-force clamping cylinder, pneumatic brake, hydroforming fixture, or injection mold degating unit) required 12 to 16 bar of operating pressure, plant engineers were forced to elevate the entire plant-wide ring line from 6 bar to 12+ bar.
Thermodynamically, raising an entire centralized compressor network by just 1 bar (14.5 psi) incurs an approximate 7% to 10% surge in compressor electrical power consumption, while exponentially increasing line-leakage losses across thousands of meters of piping. In compliance with DIN EN ISO 50001 Energy Management Systems, modern German plant engineers are transitioning away from high-pressure centralized grids. Instead, they run baseline central ring lines at an energy-conservative 5 to 6 bar, while deploying localized, decentralized air pressurized booster pumps (Druckluftverstärker) directly at the machine workstation to amplify local pressure up to 16, 25, or 40 bar on demand.
The Engineering Reality of German Point-of-Use Pneumatics
By boosting air pressure solely at the designated point-of-use rather than over-pressurizing the entire shop floor, German production facilities eliminate up to 75% of pneumatic distribution energy losses, protect pneumatic valve lifespans, and strictly satisfy the audit criteria enforced by the Federal Office for Economic Affairs and Export Control (BAFA) energy audits.
Engineering Compliance for the German Machine Directive
Octagon's air pressurized booster pumps are purpose-engineered to integrate seamlessly within European CE, DIN, and VDMA regulatory frameworks.
PED 2014/68/EU & CE Machinery
All pressure-retaining cylinders, accumulator vessels, and manifold blocks comply strictly with the European Pressure Equipment Directive (PED) and CE Machinery Directive 2006/42/EC. Each booster station ships with full Declaration of Conformity and Material Test Reports (EN 10204 3.1).
ATEX Explosion Proofing (Directive 2014/34/EU)
Because Octagon air booster pumps operate entirely without electrical coils, switches, or motors, they generate zero frictional electrical sparking. They are inherently suitable for volatile, paint-spraying, chemical processing, and explosive ATEX Zone 1 / Zone 2 environments.
DIN EN ISO 4414 Fluid Power Standards
Equipped with metric G-thread and NPT-thread interchangeable porting, integrated exhaust silencing to meet German workplace noise regulations (<72 dB(A)), and failsafe automatic shut-off logic that balances output pressure dynamically against preset setpoints.
2. Architecture Comparison: Octagon Decentralized Booster vs. Traditional Compressors
Procurement directors and plant engineering teams frequently evaluate whether to install dedicated secondary screw compressors or deploy localized pneumatic intensifiers. The following matrix illustrates the technical and lifecycle metrics under typical German operational criteria.
| System Parameter | Octagon Pneumatic Booster Station | Dedicated High-Pressure Screw Compressor | Central Plant Line Overpressurization |
|---|---|---|---|
| Capital Investment (CapEx) | Low (15% to 25% of dedicated machine) | Very High (€18,000 – €45,000+ unit cost) | Extreme (Entire infrastructure rebuild) |
| Electrical Power Requirement | 0 kW (Utilizes existing 5-bar shop air) | 7.5 kW – 37 kW continuous motor draw | Multiplies whole-plant kW consumption |
| Installation Footprint | Compact skid (under 0.3 m² machine-side) | Large dedicated compressor room required | Distributed piping network alterations |
| Thermal & Heat Dissipation | Cold exhaust; adiabatic cooling effect | Severe; requires active oil/air chilling | Severe building heat load increase |
| Explosion Proof (ATEX) | Inherently Safe (100% pneumatic) | Requires expensive explosion-proof motors | Presents line-rupture safety hazards |
| Maintenance Downtime | Seal cartridge replacement < 30 minutes | Oil changes, separators, valve overhauls | Entire plant shutoff during line maintenance |
Taiwan Precision R&D with Scaled Supply Chain Mastery
How Octagon bridges German precision tolerances with flexible, cost-optimized production agility.
Taiwan Engineering Rigor & ±0.002 mm Tolerancing
Founded in 2008 in Taoyuan City, Taiwan, Octagon Precision Mold brings over 15 years of high-precision mold-making and micro-machining expertise to fluid power engineering. The heart of any air booster pump lies in its directional spool valve and high-pressure piston seals. Even micro-scale dimensional variances cause pressure blow-by, cycle stalling, and premature seal breakdown.
Every critical valve bore, piston sleeve, and pilot rod in Octagon air booster systems is honed to tolerances of ±0.002 mm with a mirror surface finish of Ra 0.05 – 0.2 μm. This ultra-low surface roughness minimizes seal friction, permitting continuous cycling under non-lubricated conditions, ensuring pure oil-free compressed air delivery compliant with cleanroom and automotive paint-booth requirements.
Robust Supply Chain Agility & 100% FAT Testing
While our R&D and engineering governance stem from Taiwan, our scaled production facilities in mainland China provide German Tier-1 suppliers and mechanical engineering firms (Maschinenbau) with unmatched supply chain resilience. With 45+ registered patents and an engineering workforce averaging over a decade in pneumatic R&D, we manufacture customized boosters, accumulator skids, and valve blocks with short 2-to-3-week dispatch lead times.
Every single air booster pump destined for Germany undergoes rigorous Factory Acceptance Testing (FAT): 100% helium/air pressure decay leak-rate verification, cycling response calibration under fluctuating inlet pressures (2 bar to 8 bar), and maximum stall pressure holding tests up to 1.5x nominal rating.
Mission-Critical Use Cases Across Germany's Key Industrial Hubs
From Bavarian CNC machining centers to Swabian automotive die-casting and Rhine-Ruhr steel equipment.
Automotive Tooling & Clamping (Stuttgart / Wolfsburg)
Hydraulic clamping cylinders on automated car chassis welding lines require instant high clamping forces. Octagon SWP-02A and SWP-7.5 series pumps amplify standard 6-bar plant air to 12–25 bar to deliver high-tonnage locking force without bulky hydraulic power units.
Precision In-Mold Cutting & Degating (Bavaria & Hesse)
For precision plastic injection molding in medical and consumer electronics, in-mold gate cutting demands rapid, high-pressure actuation while the tool is closed. Our air booster stations drive micro-cylinders that cleanly trim runner gates inside the mold cycle.
Gas Pipeline & Valve Pressure Proofing (NRW / Ruhr)
German valve manufacturers and piping fabricators utilize Octagon high-ratio booster units for hydrostatic and pneumatic burst pressure testing. Booster units precisely maintain static test pressures up to 40 bar with zero drift and automatic stroke recovery.
CNC Machining Tool Changers & Spindles (Baden-Württemberg)
High-torque CNC machining centers often require 10 to 16 bar to eject heavy HSK tooling tapers from high-speed spindles during tool exchange. Octagon compact air boosters integrate straight into the machine column without redesigning electrical wiring.
Laser Cutting Assist Gas & Purging (Saxony & Thuringia)
Fiber laser cutting systems need elevated gas pressure to cleanly expel slag from thick stainless steel plate cuts. Installing an Octagon pneumatic gas booster provides exact pressure stability, eliminating rough kerf cuts caused by plant air fluctuation.
Cleanroom Food Packaging & Bottling (Hamburg / Lower Saxony)
Pneumatic blow molding, seal-capping, and leak detection testing in food & pharma packaging lines benefit from our 100% oil-free booster chambers. Stainless steel options prevent corrosion during aggressive washdown cycles.
Frequently Asked Questions by German Engineering Procurement
Technical guidance covering flow rates, maintenance protocols, duty cycles, and integration requirements.
How does an air-pressurized booster pump function without electrical power?
What is the typical lifecycle of the dynamic piston seals, and are replacement kits readily stocked?
Can Octagon booster pumps handle gases other than ambient compressed air (e.g., Nitrogen or Argon)?
How does the booster maintain pressure when the downstream system stalls or reaches target pressure?
What compressed air filtration quality is required at the inlet?
What documentation is provided for German CE compliance and plant safety audits?
Octagon Industrial Pneumatic & Booster Product Matrix
Explore our complete line of industrial air booster pumps, heavy-duty gas intensifiers, and high-precision stamping tooling components trusted across 60+ countries.

OEM Octagon SWP-7.5 Industrial Performance Air Booster Pump
Engineered for extreme performance demanding continuous cycling under heavy industrial loads, offering robust heat dissipation and low cycle degradation.
Inquire Specs & RFQ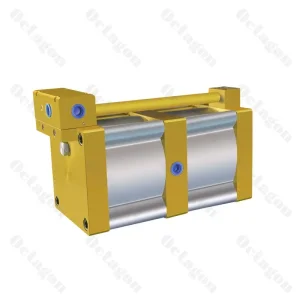
ODM Octagon High-Reliability Air Booster Pump Station
A dependable, quiet-running pneumatic booster solution customized with tailored mounting footprints to fit inside European compact automated cells.
Inquire Specs & RFQ
High-Quality Octagon SWP-02B-G Pneumatic Air Booster Pump
Equipped with integrated dual-stage exhaust silencing and high-flow check valves, matching German noise safety and high flow recovery requirements.
Inquire Specs & RFQ
High-Quality SWP-05 High-Efficiency Air Booster Pump
Delivers a five-fold pressure multiplication ratio, enabling production lines with a standard 6-bar supply to drive 30-bar pressure testing and clamping tasks.
Inquire Specs & RFQ
Precision SWP-05-G Gas & Air Booster Pump Station
Constructed with high-strength anodized aluminum cylinder barrels and stainless steel piston shafts for corrosion-free continuous industrial cycling.
Inquire Specs & RFQ
Custom Precision Stamping Die Components for German Plants
Ultra-precision punches, guide bushings, and stamping die components machined to ±0.002 mm tolerance, seamlessly pairing with booster-driven press lines.
Inquire Specs & RFQ
Octagon SWP-05-G High-Delivery Compressed Air Booster System
High-displacement air booster system optimized for rapid pressure vessel pre-filling, pipe burst testing, and multi-station clamping manifolds.
Inquire Specs & RFQ
ODM Octagon SWP-7.5 Continuous Duty High-Pressure Booster
The flagship heavy-duty air-driven booster pump delivering reliable, continuous output up to 40 bar with minimal maintenance overhead for German engineering partners.
Inquire Specs & RFQ