
Precision Mold Inserts, Power Intensifiers & Industrial Assemblies
Discover our primary export-grade solutions engineered for high-tonnage injection moulding, automated degating, and precision signal integration across aerospace, automotive, and medical platforms.








Global Landscape of High-Tonnage Large-Part Injection Moulding
The industrial market for large-part plastic injection moulding has shifted from basic commodity molding to mission-critical, structural engineering. Driven by the aggressive lightweighting directives in electric mobility (EVs), massive renewable energy infrastructure enclosures, aerospace interior cabins, and heavy commercial vehicle logistics, multi-ton injection tools demand unprecedented clamping forces between 1,200 and 4,500 metric tons.
Massive Tonnage & Clamping Dynamics
Molding massive front fascias, truck battery covers, and mega-pallet structures requires clamping platen rigidity that resists micro-deflections under cavity pressures exceeding 1,200 bar, preventing parting line flashing and structural sink marks across 2-meter projected areas.
1,200T - 4,500T MachinesThermodynamic Warpage Control
Large surface areas suffer extreme volumetric shrinkage variations. Integrating multi-zone conformal cooling channels and high-pressure hot runner valve gates ensures balanced melt flow fronts, cutting residual stress and holding dimensional planar warpage within <0.8 mm across total length.
Conformal CFD SimulationClosed-Loop Precision In-Mold Degating
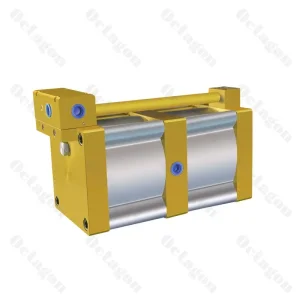
Post-mold manual gate trimming on large components introduces human inconsistency and micro-cracking. Octagon integrates pneumatic and gas-liquid intensifier booster systems within the tool, delivering 7,000 kgf of force to cleanly shear gates while the platen is locked.
Automatic Zero-Burr CutIndustry Development Trends Shaping the Next Decade
Modern tier-one manufacturing programs require large molders and component exporters to move beyond traditional tool-and-die paradigms into AI-driven closed loops, smart sensory tooling, and circular polymer engineering.
MuCell & Chemical Microcellular Foaming
Supercritical N2 or CO2 gas injection reduces bulk component density by 10% to 25% in thick-wall automotive dash carriers and industrial bins without sacrificing structural flexural modulus.
Lightweighting TechDigital Twin & Real-time Cavity Analytics
Piezoelectric pressure transducers and infrared melt front sensors embedded behind tool inserts relay live rheology curves to the injection controller, actively auto-adjusting switchover points per cycle.
Industry 4.0 IoTHigh-Pressure Assist & Sequential Gating
Employing specialized gas booster pumps (e.g., SWP and SWB series) enables rapid nitrogen gas-assist coring, eliminating sink marks in ultra-thick ribs and reducing required machine clamping tonnage by 35%.
Gas-Assist MoldingPost-Consumer Recyclate (PCR) Optimization
With ESG mandates demanding up to 50% PCR content, our hardened bimetallic barrels and tool steel coatings withstand higher abrasive filler ratios while sustaining uniform thermal conductivity.
Circular PolymersMission-Critical Applications Across Global Geographies
Whether shipping oversized injection molds to North American automotive hubs or supplying fully assembled medical housing enclosures across Western Europe, Octagon satisfies regional engineering standards with native compliance.
Automotive Front Fascias & Underbody Shields
Regional Focus: North America & Germany (OEM Tier 1). Parts measure up to 2,200 mm in span. We provide hot runner sequential injection tooling with mirror finishes (Ra 0.05μm) guaranteeing class-A painted exterior aesthetics and zero witness lines.
PP-EPDM-T20 & TPOEnergy Storage Enclosures & EV Battery Trays
Regional Focus: East Asia & Nordic Europe. Heavy structural battery cell cradles and thermal insulation covers. Integrated with flame retardant UL94-V0 compliance, tight internal rib geometry, and automated high-pressure harness channel integration.
PA66-GF30 & PBT V0Large Medical Diagnostics & Imaging Chassis
Regional Focus: USA, Switzerland & Japan. Structural MRI/CT scanner exterior panels and mobile cart chassis. Engineered under ISO 13485 cleanroom validation with zero volatile plasticizer outgassing and chemical disinfectant immunity.
Medical PC/ABS & PVDFEngineering Benchmark Matrix: Standard vs. Octagon Large-Part Solutions
Compare our industrial tool design parameters and automated processing controls against conventional commodity injection export houses.
| Performance / Tooling Metric | Commodity Injection Exporters | Octagon Precision Engineering System | Production Advantage |
|---|---|---|---|
| Machining Tolerance | ±0.02 mm to ±0.05 mm | ±0.002 mm (CNC optical grinding) | Eliminates parting line flash & mismatch |
| Surface Polishing | Ra 0.4 – 0.8 μm (SPI B1) | Ra 0.05 – 0.2 μm (SPI A1 Mirror) | Zero drag marks on deep draw walls |
| Gate Trimming Process | Manual knife cut / Off-line robotic cell | In-Mold Hydraulic/Air Boost (7,000 kgf) | Zero secondary labor, cycle reduced 4-8s |
| Pressure Boost Generation | Standard workshop air (6–8 bar) | Dedicated Booster (SWP/SWB series) | Consistent peak 160+ bar fluid pressure |
| Mold Steel Longevity | P20 (300,000 to 500,000 shots) | 1.2343 ESR / S136 / Nak80 (1,000,000+ shots) | Reduced maintenance & replacement cost |
| Wiring & Subassembly Integration | Third-party outsourced harness | Proprietary In-House Harnessing | 100% point-to-point continuity tested |
Octagon Large-Component Technology Roadmap
Rigorous analysis of weld line positioning, shear-rate-induced degradation, fiber alignment in glass-reinforced resins, and venting calculations under 3,000T clamping.
Utilizing Makino and Sodick high-speed machining centers to profile massive mold cores up to 25 metric tons with micron-level kinematic accuracy and conformal cooling drillouts.
Direct integration of Octagon patented SWB intensifier pumps and high-pressure timing cabinets, executing instantaneous gate severing before the mold parting surface cracks.
Full Zeiss laser coordinate measuring machine (CMM) dimensional reports, colorimetric surface map comparisons against native CAD, and full PPAP Level 3 documentation for export delivery.
Macro Industry Solutions: Bridging Taiwan Precision with Scalable Production
Established in 2008 in Taoyuan, Taiwan, Octagon combines Taiwanese metrology discipline and patent-backed automation engineering with scaled manufacturing facilities in mainland China. We provide a single-source ecosystem eliminating supply chain fragmentation.
One-Stop Multi-Category Integration
Why coordinate three separate suppliers for injection tooling, pneumatic booster pumps, and electrical cable harnesses? Octagon manufactures the entire assembly, delivering plug-and-play functional modules to global assembly plants.
Turnkey HardwarePatented In-Mold Cutting Systems
Protected by 45+ registered patents, our high-pressure timing cabinets and intensifiers eliminate mechanical gate vestige, allowing direct shipment of injection molded components to cleanroom paint and final packaging lines.
45+ Registered PatentsDefect-Free Global Logistics
Oversized molds and structural components are packed in certified climate-resistant maritime crates with desiccants, nitrogen purging, and digital shock sensors. Complete documentation guarantees rapid customs clearance across 60+ countries.
Export Ready PackagingExpert Answers for Global Procurement & Mold Engineering Teams
Detailed clarifications on machine tonnages, dimensional tolerances, material selections, and turnkey delivery protocols for global injection moulding projects.
What machine tonnage range and maximum part dimensions can Octagon accommodate?
How does Octagon control thermal warpage and dimensional sink on large-surface moldings?
What are the key technical advantages of Octagon's patented in-mold cutting automation?
Can Octagon provide custom wiring harnesses and pneumatic booster systems as a packaged assembly?
What quality certifications and metrology reports accompany export shipments?
High-Performance Booster Systems, Sprue Bushings & Wiring Solutions
Expanding your industrial throughput: Reliable pneumatic boosters, CE-certified mold components, and specialized wiring harnesses engineered to ensure zero downtime in high-duty operations.




Collaborate with Octagon Senior Mold & Automation Specialists
Submit your component 3D models (STEP, IGES, Parasolid) or engineering drawings. Our engineering team conducts initial DFM analysis, mold flow simulation, and gate optimization within 24 hours.